Automatic Adhesive Dispensing Machine Insights: Beads, Dots, Spray, Potting, and Encapsulation
Automatic adhesive dispensing machines apply controlled amounts of adhesives, sealants, coatings, and resins with greater repeatability than manual application.
The right system depends on the material, required pattern, target volume, substrate, production speed, and quality standards.
What Is Automatic Adhesive Dispensing?
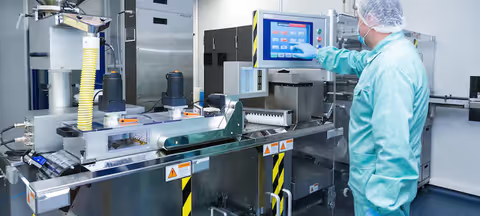
An automatic adhesive dispensing system moves a dispensing head along a programmed path while a pump, valve, or jetting system delivers a measured amount of material. It can apply adhesive as beads, dots, lines, sprays, fills, or encapsulants.
A typical system includes:
Material supply: Cartridge, syringe, pressure pot, drum, or bulk supply system.
Metering unit: Controls the amount of material delivered.
Dispense valve or pump: Regulates flow and deposit size.
Motion system: Robot arm, gantry, or XY table that moves the dispensing head.
Controls: PLC, teach pendant, vision system, and recipe management.
Inspection: Camera, laser profiler, or weight-check system to verify bead presence and dimensions.
Curing system: UV lamp, oven, heat source, or ambient-curing area, depending on the adhesive.
Automation improves consistency, reduces waste, increases throughput, and lowers dependence on operator skill.
Bead Dispensing
Bead dispensing applies a continuous line or bead of adhesive along a path. It is commonly used for bonding, sealing, gasketing, and structural assembly.
Typical applications include:
Form-in-place gaskets
Automotive sealing and bonding
Appliance assembly
Electronics enclosure sealing
Glass and metal bonding
Structural adhesive application
A round nozzle generally creates a round bead, while nozzle speed, material viscosity, dispense pressure, and standoff height affect bead width, height, and continuity. Consistent bead geometry is essential for sealing performance and joint strength.
Dot Dispensing
Dot dispensing places precise, discrete amounts of adhesive at defined locations. It is ideal when only small, controlled deposits are needed rather than a continuous line.
Common uses include:
Surface-mount component bonding
Underfill for electronic components
Small-part assembly
Label or gasket attachment
Sensor bonding
Microelectronics and PCB assembly
Jetting valves are often used for very small dots because they dispense droplets at high speed without touching the substrate. This reduces contamination risk and is useful for sensitive electronic components. Volumetric pumps generally provide more repeatable dot volumes than basic time-pressure systems.
Spray Dispensing
Spray dispensing atomizes adhesive, coating, primer, or sealant into a fine mist or controlled pattern. It is used when broad, thin, and uniform coverage is required.
Typical applications include:
Conformal coating of circuit boards
Primer application before bonding
Gasket coating
Protective coatings
Thin adhesive layers
Large-surface sealing
Spray systems require careful control of nozzle type, air pressure, fluid pressure, standoff distance, and robot speed. Fan-spray nozzles create wide, thin coverage, while other nozzle designs can create narrower patterns. Proper ventilation, filtration, and overspray management are essential.
Potting
Potting fills a cavity or enclosure with a protective resin, usually an epoxy, silicone, or polyurethane. The goal is to protect electronic components, sensors, connectors, or assemblies from moisture, vibration, dust, chemicals, and thermal stress.
Common potting applications include:
LED drivers and power supplies
Sensors and transducers
Automotive electronic control units
Connectors and cable assemblies
Industrial controls
Battery modules and EV components
For potting, the system must control fill volume, flow rate, air entrapment, and cure conditions. Vacuum degassing, controlled dispensing, and proper material preparation help reduce bubbles, voids, and incomplete coverage.
Encapsulation
Encapsulation covers a component or assembly with a protective layer of resin. Unlike potting, which fills an entire cavity, encapsulation may coat or surround a specific component while leaving other areas exposed.
Typical uses include:
Protecting chips, coils, and sensors
Insulating electronic components
Improving resistance to moisture and vibration
Providing mechanical reinforcement
Protecting components from chemicals or contamination
Encapsulation is widely used in electronics because it can extend component service life and improve reliability. The material must match the component’s thermal expansion, electrical insulation needs, and operating environment.
Choosing a Dispensing Method
| Method | Best For | Material Pattern | Key Consideration |
|---|---|---|---|
| Bead dispensing | Bonding, sealing, gaskets | Continuous line | Bead width, height, and continuity |
| Dot dispensing | Small components and precise bonding | Discrete deposits | Dot volume and placement accuracy |
| Spray dispensing | Coatings, primers, thin layers | Mist or fan pattern | Overspray and uniform coverage |
| Potting | Filling cavities and protecting electronics | Full cavity fill | Air bubbles, viscosity, and cure |
| Encapsulation | Covering selected components | Controlled coating or fill | Coverage, insulation, and protection |
Selecting the Right Equipment
Choose the dispensing technology based on the material and process requirement—not only on machine price.
| Technology | Best Materials | Typical Use |
|---|---|---|
| Time-pressure dispenser | Low- to medium-viscosity fluids | Basic dots, beads, and filling |
| Auger or screw pump | Medium- to high-viscosity materials | Consistent dots and beads |
| Gear pump | Many viscosities; stable volumetric output | Precision production dispensing |
| Progressive cavity pump | Silicones, polyurethanes, filled epoxies | Gaskets, beads, potting |
| Piston dispenser | Calibrated shots | Precision dots and small fills |
| Jetting valve | Low-viscosity fluids | Fast, non-contact micro-dots |
| Two-component meter-mix system | Two-part epoxies, silicones, polyurethanes | Potting, encapsulation, structural bonding |
Two-part materials require accurate mixing ratios. A meter-mix system measures and combines the base resin and hardener before dispensing, helping maintain consistent cure and mechanical performance.
Material Factors That Affect Dispensing
Before selecting a machine, evaluate the adhesive’s:
Viscosity: Thin fluids may drip or spray; thick materials may need pumps or heated systems.
Rheology: Shear-thinning materials can behave differently at different flow rates.
Cure method: UV, heat, moisture, room temperature, or two-part chemical curing.
Pot life: The usable working time after mixing.
Fillers and abrasiveness: Filled materials may wear valves, needles, and pumps.
Temperature sensitivity: Heating or cooling may be needed to maintain stable viscosity.
Bubble tendency: Degassing may be needed before potting or encapsulation.
Shelf life and storage: Some adhesives require refrigeration or controlled humidity.
Quality Control and Inspection
Automated dispensing should include checks that catch defects before they become product failures.
Useful controls include:
Vision inspection for bead presence, width, and position
Laser profiling for bead height and continuity
Weight checks for potting or fill volume
Pressure and flow monitoring
Void and bubble detection for encapsulated parts
Cure verification through UV dose, temperature, or hardness testing
Data logging for traceability and process improvement
Inline inspection can automatically route defective parts to rework or rejection and record dispense parameters for quality audits.
Common Problems and Solutions
| Problem | Likely Cause | Solution |
|---|---|---|
| Inconsistent bead width | Varying pressure, speed, or viscosity | Use volumetric dispensing and stabilize material temperature |
| Missing dots | Clogged nozzle or air in fluid line | Prime the system, filter material, and inspect nozzles |
| Air bubbles in potting | Poor degassing or fast dispensing | Vacuum degas material and control fill rate |
| Dripping after dispense | Incorrect valve closing or material too thin | Adjust valve settings or change valve type |
| Uneven spray coverage | Wrong nozzle, pressure, or standoff distance | Optimize spray parameters and robot path |
| Poor adhesion | Contaminated surface or wrong pretreatment | Clean, plasma-treat, prime, or abrade the surface |
| Cure failure | Incorrect mix ratio or insufficient cure energy | Verify meter-mix accuracy and curing conditions |
Maintenance and Safety
Regular maintenance keeps dispensing accurate and prevents downtime.
Maintenance tasks include:
Clean nozzles, valves, and fluid lines according to the adhesive’s cure schedule.
Replace worn needles, seals, pistons, and pump components.
Check for leaks, air bubbles, and pressure instability.
Calibrate dispensing volume and bead geometry.
Inspect robot paths, fixtures, and vision systems.
Keep spare valves, nozzles, filters, and seals available.
Follow manufacturer guidance for flushing two-part systems before material cures.
Safety practices include using appropriate ventilation, protective equipment, grounding, spill containment, and manufacturer-approved cleaning chemicals. Some adhesives and solvents require special handling due to flammability, skin sensitivity, or respiratory hazards.
Best Practices for Implementation
Start with a process trial using production-representative parts and materials.
Define target bead width, dot volume, coverage, cure time, and inspection criteria.
Match the pump or valve to the adhesive’s viscosity and rheology.
Use fixtures that locate parts consistently.
Program robot speed and Z-height to maintain uniform deposits.
Validate the process with statistical measurements, not just visual inspection.
Train operators on priming, cleaning, material handling, and fault recovery.
Monitor quality data continuously and adjust before defects become widespread.
Automatic adhesive dispensing is most effective when material selection, dispensing hardware, robot motion, curing, and inspection are designed as one integrated process. Whether applying beads, dots, spray coatings, potting compounds, or encapsulants, controlled automation improves repeatability, reduces waste, and supports higher product reliability.